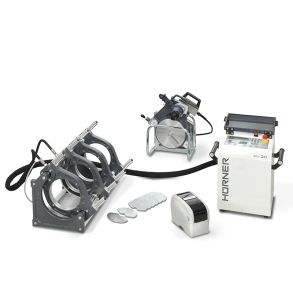
HÜRNER HWT 630 CS servo-operated workshop system for manufacturing PE,
PE 100 RC, PP, and PVC-U, PVC-C pipes,
segmented bends, and fittings, fitted with
narrow aluminum master clamps.
The design of the machine is such that pipes and
segments up to O.D. 630 mm / 24“ with any
SDR ratio up to SDR 9 can be processed.
The system was developed under the machinery
directive 2006/42/EC as amended and is set on
a welded and bolted, totally heavy‑duty support
frame resistant to warping by design. Both the
movable carriage of the system and the console
carrying the heating element and the facing tool
travel on precision‑engineered, heavy load‑bear‑
ing trapeze‑shaped guides constructed with
smoothly travelling runner blocks.
A pneumatic cylinder will remove the heating
element from in-between the components in no
time, enabling change-over in as short as 2 se‑
conds. The facing tool assembly, too, is inserted
and removed automatically.
The swiveling master clamps on both sides can
be rotated by up to 2 × 22.5 deg. and also fea‑
ture horizontal and vertical adjustability, to allow
for compensating any misalignments.The facing
tool has a rugged chain drive mechanism and is
inserted and fastened between the component
butts as easy as ABC thanks to a gas-pressure
cylinder.
The heating element temperature control and
the application of the welding force precisioncontrolled by a servomotor are performed in
compliance with the standard applicable to the
operation (DVS, UNI, WIS, NEN, etc.).
All welding parameters critical for a high-quality
and reproducible welded joint, it goes without
saying, are monitored for the entire welding
process and saved to one of the 10,000 welding
reports the system memory holds.
In its standard delivery, the machine features a
high-resolution color display touchscreen. This
device allows entering and displaying both all
required component parameters and the needed
traceability information.
A unique feature in the field of butt welding that
this system version offers is the user access man‑
agement using RFID technology for foolproof
and extremely convenient input of the data into
the system, rather than the bar code and scan‑
ning pen that have been common.
Also a revolution in workshop machines is the
possibility of preheating by means of a preheat‑
ing cylinder.
As with all HÜRNER CNC systems, a USB
interface port is also provided for downloading
the welding data to a USB stick as a PDF abstract
or extended report or for archiving them in the
HÜRNER DataWork Professional format. Com‑
bining this to HÜRNER WeldTrace app, which
has QR code scanning from label tags imple‑
mented, tracing back any and all welding and
project data flawlessly is guaranteed even years
after the work was completed. The welding data
can also be transferred via the in-house LAN /
Wi-Fi network to a printer or to the DataWork
database software.
HÜRNER HWT 630 CS control system specs
Automatic data logging 10,000 welding operations
Data input Touchscreen, RFID reader, scanner (optionally)
System self-monitoring System check, Computerized maintenance management including logging
Welding monitoring system Welding forces, welding times, ambient temperature, memory control, heating element temperature
Standard-compliant
ISO 12176 traceability
Commission number with 32 alphanumeric characters, ISO-compliant RFID welder ID code, additional (user‑defined) data alphanumeric
characters, ISO‑compliant pipe parameters, fitting parameters, pipe length, installing company, joint number, inventory number, display of
maintaining company; supported welding standards DVS, WIS, SEDIGAS, UNI, NEN, others upon request
Data download with
print menu
USB port (USB A) for data transfer as PDF abstract or extended report to USB stick or (optional) label tag printer, incl. tag printer menu;
transfer also possible in the HÜRNER DataWork Professional database format
Working languages DE, EN, FR, NL, IT, others upon request
All components are covered by the 12-month HÜRNER warranty